


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
 Send Inquiry
 0804580361308045803613

 Send Inquiry
500 LPH RO Mineral Water Plant
MOQ : 1 Unit
500 LPH RO Mineral Water Plant Specification
- Water Out Conductivity
- <20 S/cm (Microsiemens/cm)
- Technology
- Reverse Osmosis (RO)
- Pump Type
- High Pressure Pump (SS)
- Feature
- PLC controlled operation, Digital Panel, Skid Mounted, Low Maintenance, High Recovery
- Frequency
- 50 Hz
- Efficiency (%)
- 98%
- Ph Level
- 6.5-8.5
- Noise Level
- < 70 dB
- Power Consumption
- 2-4 kW
- Flow Rate
- 500 LPH
- Usage & Applications
- Packaged Drinking Water, Beverages, Food Processing, Hospitals, Offices
- Recycle Rate
- 60-70%
- Product Type
- RO Mineral Water Plant
- Volume
- 500 Liters Per Hour (LPH)
- Power Source
- Electric
- Material
- Stainless Steel (SS 304/316)
- Voltage
- 220-240V AC, 50 Hz
- Water Source
- Borewell Water, Municipal Water, Ground Water
- Purity Level
- 99% removal of TDS and contaminants
- Automatic Grade
- Automatic
- Drive Type
- Electric Motor
- Filter Type
- Multigrade Sand Filter, Activated Carbon Filter, Micron Filter
- Capacity
- 500 LPH
- Installation Type
- Floor Mounted
- Raw Water TDS
- Up to 2000 ppm
- Controller Type
- Fully Automatic PLC Controller
- Output Water Usage
- Suitable for Drinking, Bottling, Food Processing
- Piping Material
- UPVC/Stainless Steel
- Storage Tank Capacity
- 500 - 1000 Litres (Optional)
- Recovery Rate
- Up to 70%
- Skid Material
- Stainless Steel/Coated MS
- Control Panel
- Digital/PLC with indicators & alarms
- Dimensions
- Approx 8 x 4 x 6 ft (L x W x H)
- Water in conductivity
- <2000 S/cm (Microsiemens/cm)
- Feed Water Pressure
- Minimum 1.5 kg/cm2 required
- Service Life of Membranes
- 2-3 years (depending on usage and feed water quality)
- No of Membranes
- 2-3 (depending on brand/model)
- System Weight
- Approx 300-450 kg
- Disinfection
- UV Sterilizer & Ozone Generator (Optional)
- Preliminary Filtration
- 5, 10, 20 Micron Pre-Filters
- Membrane Element
- Thin Film Composite (TFC) Membrane
- Automation Features
- Auto Start/Stop, Auto Flushing, Low/High Pressure Cut-offs
- Pretreatment Stages
- 3-Stage (Sand, Carbon, Micron)
- Operating Temperature Range
- 5C - 45C
500 LPH RO Mineral Water Plant Trade Information
- Minimum Order Quantity
- 1 Unit
- Supply Ability
- 1 Unit Per Month
- Delivery Time
- 7-10 Days
About 500 LPH RO Mineral Water Plant
Personalise your water purification process with the glorious 500 LPH RO Mineral Water Plant, a trending and distinguished solution for clean, safe drinking water. Engineered with celebrated thin film composite membranes, the plant features a fully automatic PLC controller and robust three-stage pretreatment system. Its stainless steel skid, digital control panel, and advanced UV/Ozone disinfection options ensure superior purity and operational excellence. Grab yours today for offices, hospitals, or food processing units and experience efficient, low-maintenance water treatment with up to 99% contaminant removal and a remarkable recovery rate.
Versatile Usage and Standout Features
The 500 LPH RO Mineral Water Plant is designed for varied usage, including packaged drinking water, food processing, offices, and hospitals. Its celebrated features such as a digital/PLC panel, high-pressure pump, skid-mounted body, and comprehensive auto automation make it ideal for demanding environments. Low-noise operation and advanced pre-filtration ensure continuous delivery of pure water, setting a new standard for industrial and commercial hydration.
Certifications, Delivery, and Export Market Reach
Estimate a seamless supply with timely delivery, supported by certified manufacturing standards. The 500 LPH RO Mineral Water Plant is widely supplied across India's main domestic market and is ready to meet export market demands. As a distinguished manufacturer, distributor, and exporter, we offer robust after-sales service, ensuring your equipment is installed and maintained efficiently, meeting celebrated and stringent quality benchmarks.
Versatile Usage and Standout Features
The 500 LPH RO Mineral Water Plant is designed for varied usage, including packaged drinking water, food processing, offices, and hospitals. Its celebrated features such as a digital/PLC panel, high-pressure pump, skid-mounted body, and comprehensive auto automation make it ideal for demanding environments. Low-noise operation and advanced pre-filtration ensure continuous delivery of pure water, setting a new standard for industrial and commercial hydration.
Certifications, Delivery, and Export Market Reach
Estimate a seamless supply with timely delivery, supported by certified manufacturing standards. The 500 LPH RO Mineral Water Plant is widely supplied across India's main domestic market and is ready to meet export market demands. As a distinguished manufacturer, distributor, and exporter, we offer robust after-sales service, ensuring your equipment is installed and maintained efficiently, meeting celebrated and stringent quality benchmarks.
FAQ's of 500 LPH RO Mineral Water Plant:
Q: How does the fully automatic PLC controller enhance plant operation?
A: The PLC controller automates and monitors all processes, from start to stop, ensures safety with alarms, and optimizes performance, reducing manual intervention.Q: What types of water sources can the 500 LPH RO Mineral Water Plant handle?
A: This plant can process borewell, municipal, and ground water sources with raw water TDS of up to 2000 ppm, ensuring versatility in installation locations.Q: Where is the 500 LPH RO Mineral Water Plant commonly installed?
A: It is ideal for hospitals, food and beverage industries, packaged drinking water facilities, offices, and other commercial establishments.Q: What is the process for maintaining the membranes?
A: Membranes typically last 2-3 years and require periodic cleaning as per water quality. Regular pre-filter replacement and system checks ensure longevity.Q: What are the main benefits of choosing this plant?
A: Key benefits include high purity (99% TDS removal), low maintenance, high recovery rate, advanced automation, and compliance with stringent domestic and export standards.Q: When can I expect delivery after placing an order?
A: Delivery timelines depend on order volume and customization but are typically estimated within a few weeks for domestic and export market supply.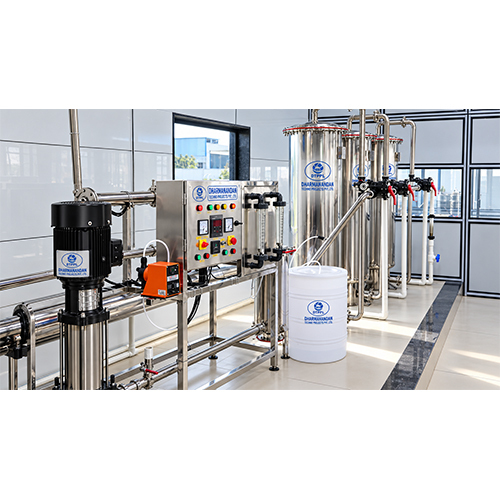
Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in RO Plant Category
Commercial Reverse Osmosis Plant
Price 120000.00 INR / Unit
Minimum Order Quantity : 1 Set
Water Source : Other, Borewell, Municipal, Surface Water
Usage & Applications : Commercial Drinking Water, Food & Beverage, Hotel, Hospital Industry, Industrial Processing
Purity Level : Up to 99%
Automatic Grade : Automatic, Other
4000 LPH RO Mineral Water Plant
Minimum Order Quantity : 1 Unit
Water Source : Other, Borewell, Municipal, River or Tap Water
Usage & Applications : Drinking Water, Bottling Plants, Hotel & Hospital Water Supply
Purity Level : 99%
Automatic Grade : Other, Automatic
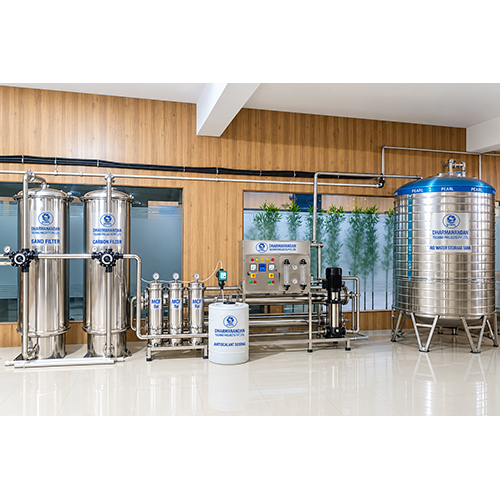
10000 LPH RO Mineral Water Plant
Minimum Order Quantity : 1 Unit
Water Source : Other, Borewell/municipal supply
Usage & Applications : Commercial and Industrial Mineral Water Packaging
Purity Level : Up to 99%
Automatic Grade : Other, Automatic
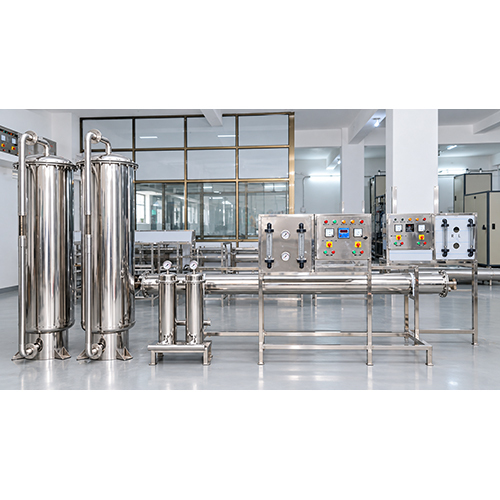
2000 LPH RO Mineral Water Plant
Minimum Order Quantity : 1 Unit
Water Source : Other, Borewell, Municipal, River, etc.
Usage & Applications : Drinking Water, Industrial, Commercial
Purity Level : Up to 99%
Automatic Grade : Other, Automatic

Contact Details
DHARMANANDAN TECHNO PROJECTS PVT. LTD.
GST : 24AADCD8174E1ZR
GST : 24AADCD8174E1ZR
For any kind of query, contact us with the details below.

- B No.166, NEAR RADHE KRISHNA RESIDENCY, KADODARA ROAD,Surat - 394327, Gujarat, India

- Phone : 08045803613
- Branch Office:
Office No. 12, Building No. A-8, Shanti Vihar CHSL, Opp. Saikrupa Hospital, Mira Road (E), Dist: Thane - 401107, Maharashtra, India

- Mr Ghanshyam B Ramani (Director)
- Mobile :08045803613
- Send Inquiry
 Send Inquiry
 Send Inquiry
 Send SMS
|


Leave a message

 |
DHARMANANDAN TECHNO PROJECTS PVT. LTD.
All Rights Reserved.(Terms of Use) Developed and Managed by Infocom Network Private Limited. |
